Company profile
The client company operates in the industrial sector and has complex mixing and transfer systems, making the use of a reliable process fluid pump essential for subsequent operational stages. The plant is equipped with stainless steel tanks, flexible connection lines and mobile systems for product transfer. This configuration allows for greater flexibility in managing the various operational stages, adapting the pump to the specific requirements of the production cycle.
- CLIENTIndustrial company specialising in fluid handling processes
- INDUSTRYIndustrial process / applications with controlled requirements
- SOLUTIONFDA-compliant pneumatic double-diaphragm pump on a mobile trolley
- MODELFDA BOXER 100
Use of the FDA BOXER 100 as a process fluid pump
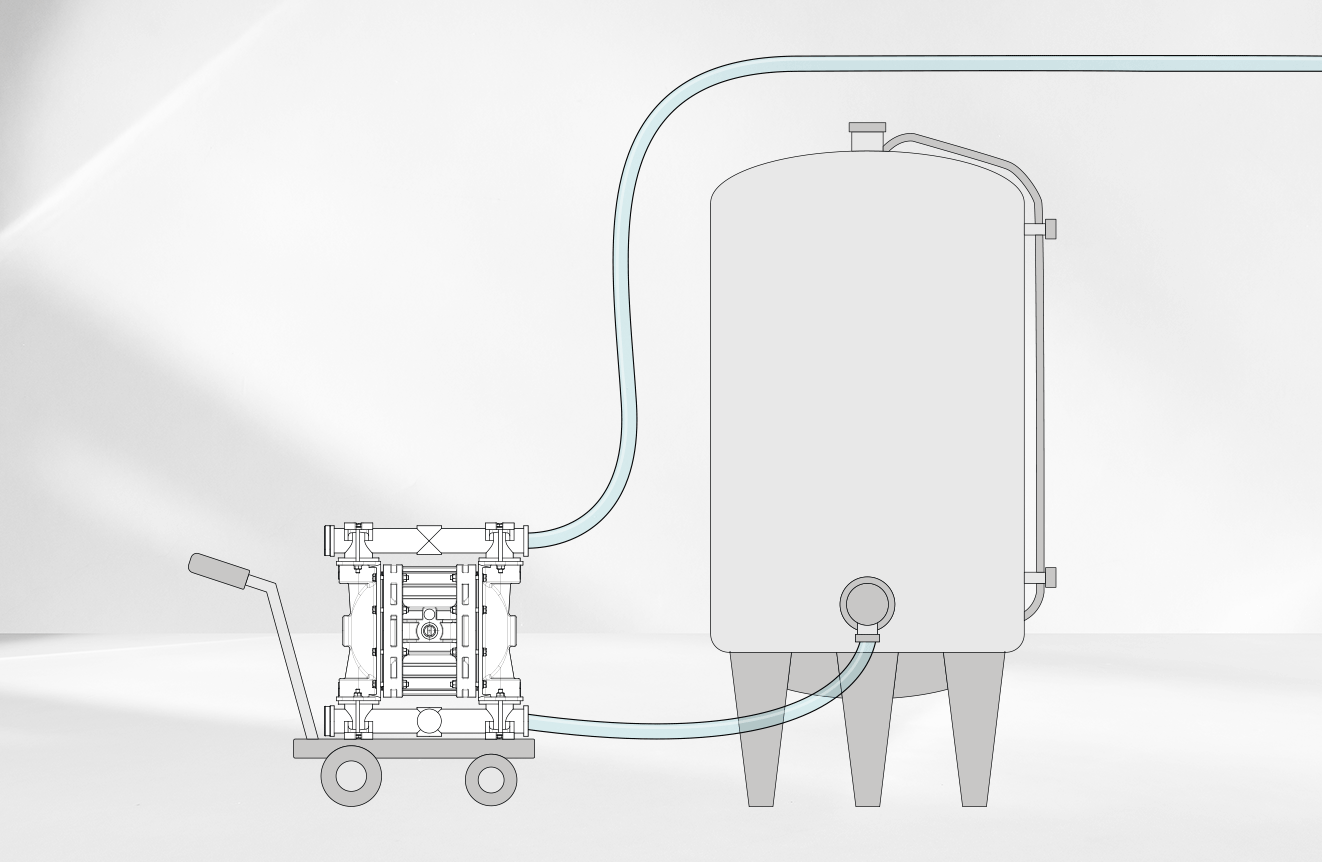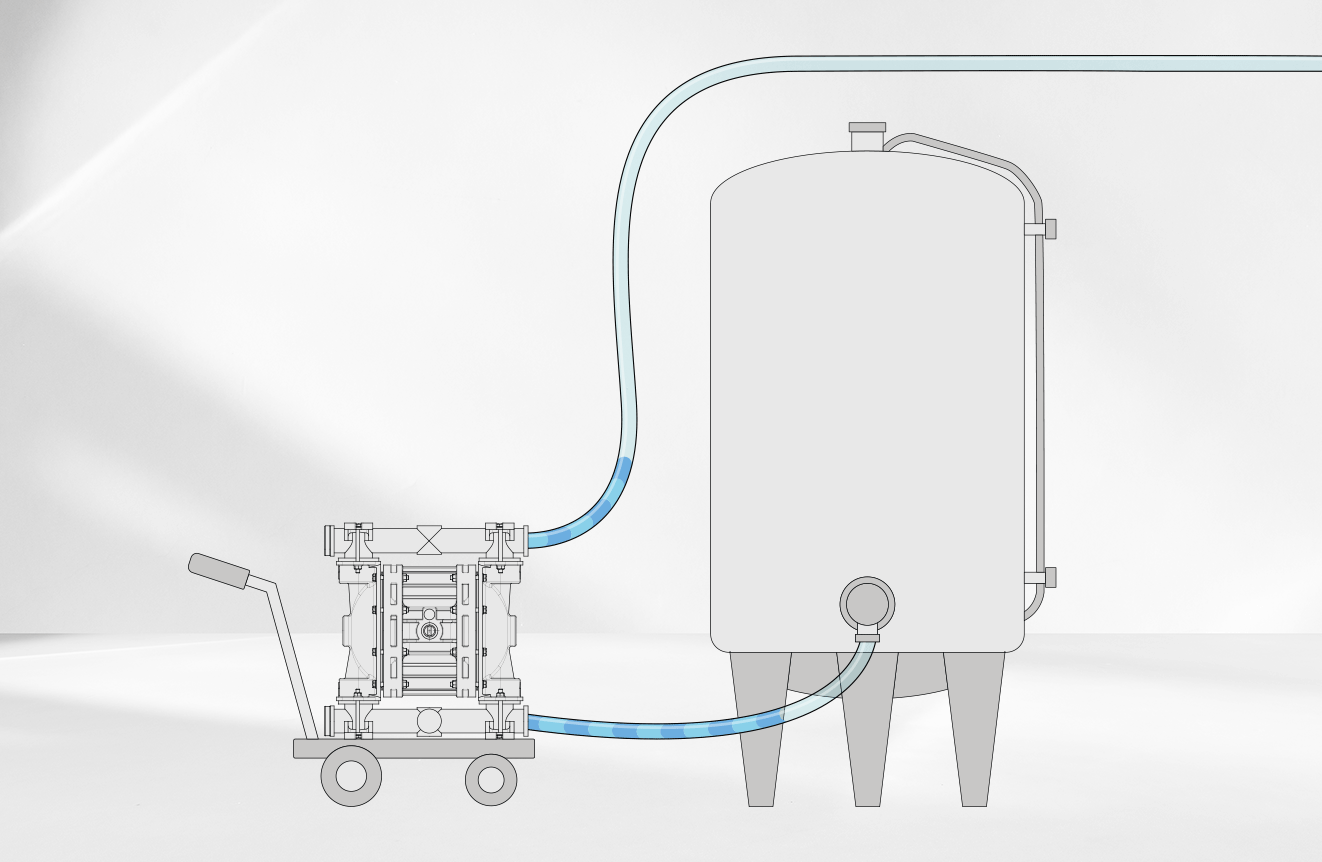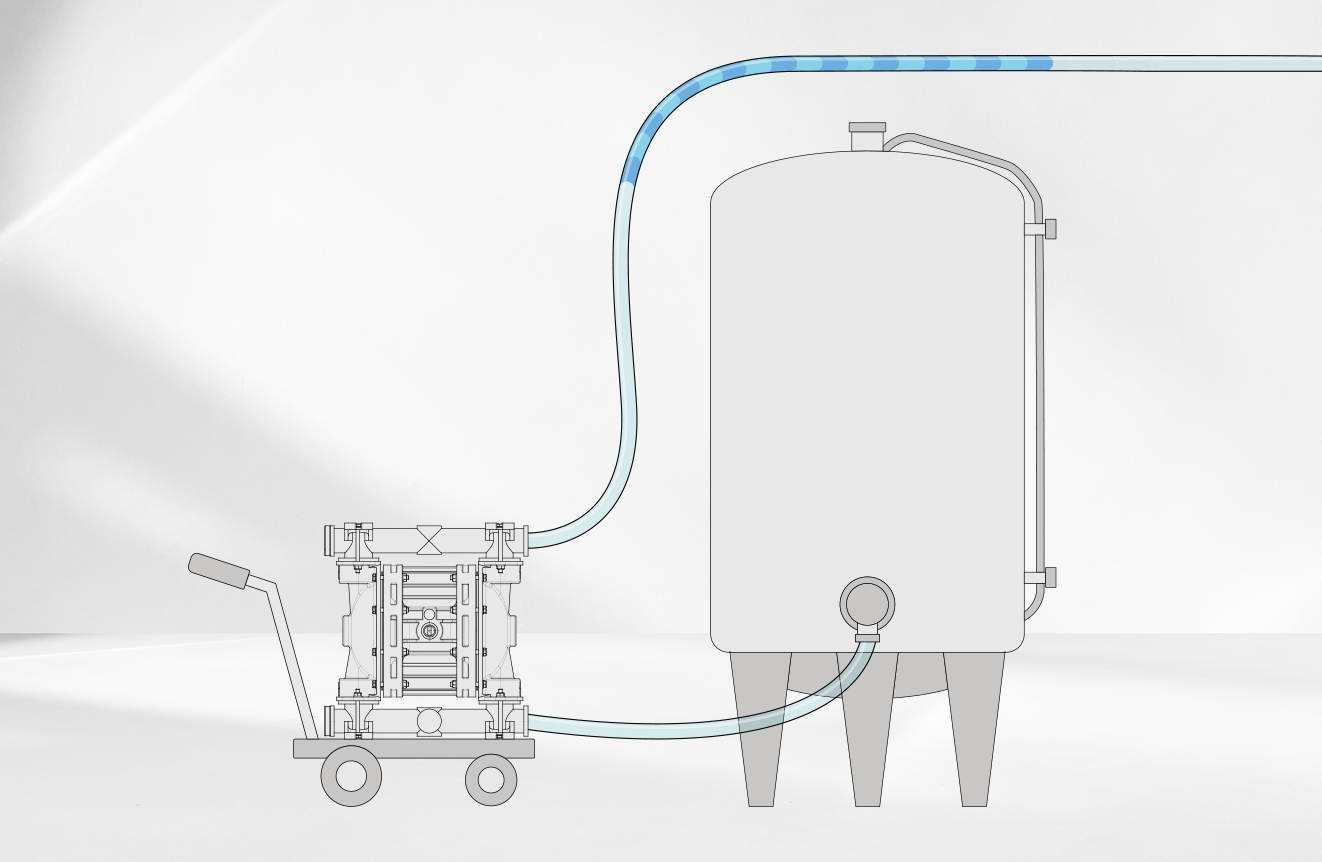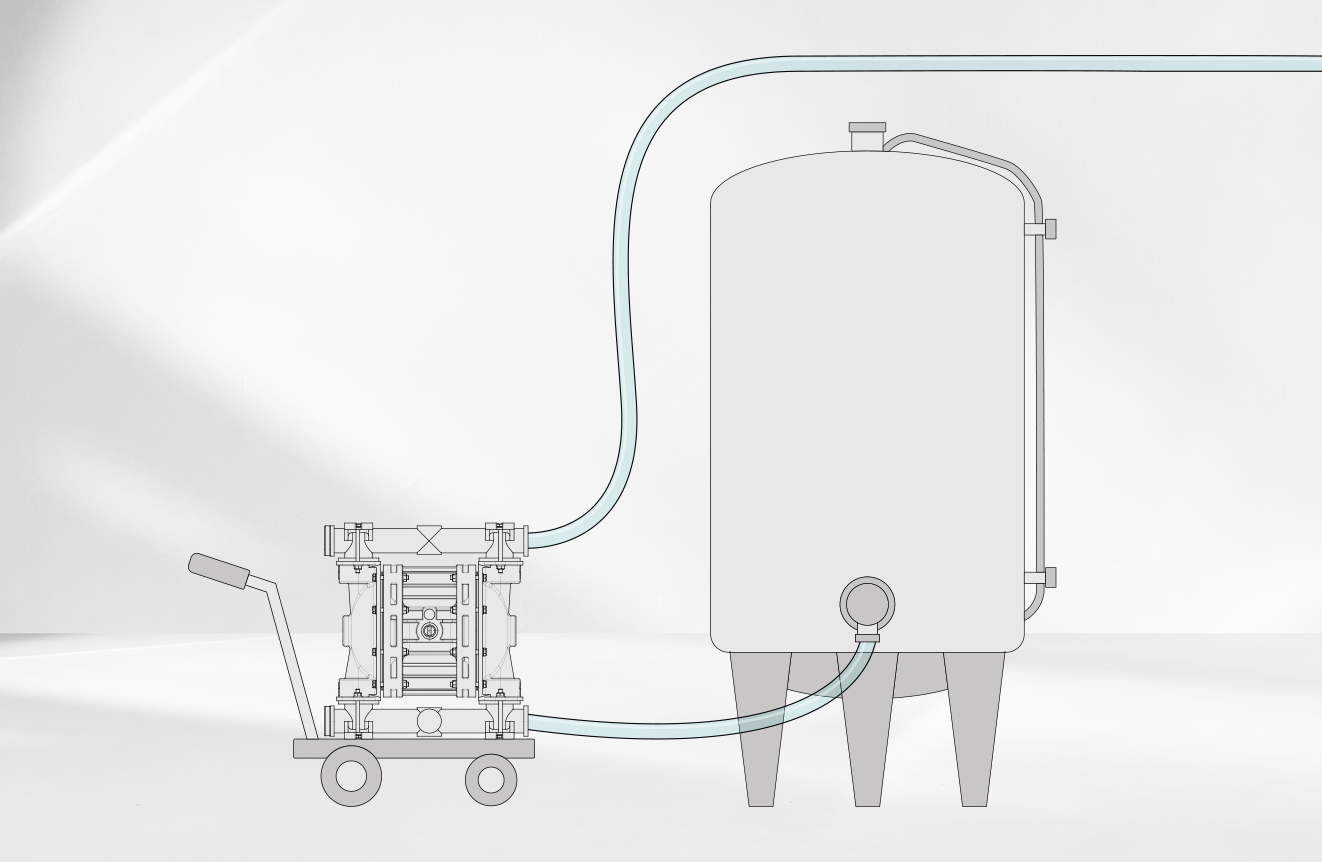
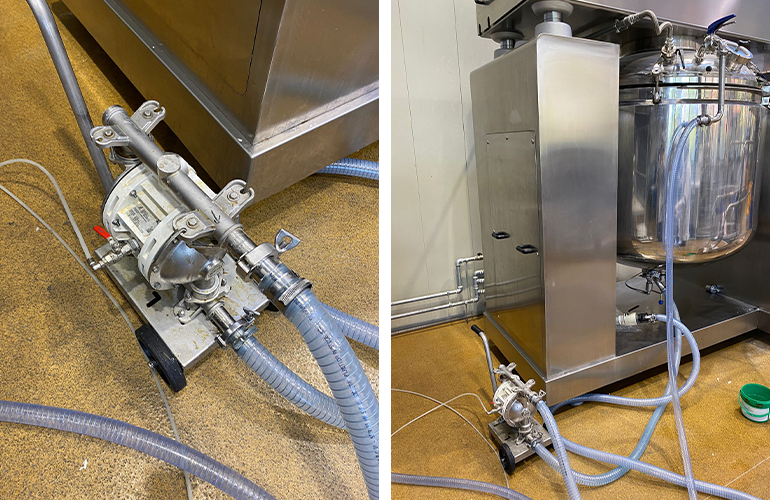
The FDA BOXER 100 is used as a pneumatic fluid pump for discharging and transferring product from tanks or process vessels to other units within the plant. The installation configuration shows that the pump is used in conjunction with flexible hoses and quick-connect fittings, a solution that allows for practical management of connection, discharge and transfer operations.
The pump is mounted on a mobile trolley, a feature that allows it to be moved easily within the production area and used at various points in the plant according to operational requirements. The double-diaphragm pneumatic technology ensures reliable fluid transfer, even under variable suction conditions or during the final stages of tank emptying.
Operating conditions of the double-diaphragm pump for waste liquids
During the plant’s operating cycle, the double-diaphragm pump for waste liquids is connected via flexible hoses to the tank or line from which the product is to be drawn. The fluid is then transferred to a subsequent collection, storage or processing area. The use of quick-connect fittings reduces connection and disconnection times, making operations easier for operators. The FDA BOXER 100 is particularly well-suited to this type of application thanks to its simple design, the self-priming capability typical of pneumatic double-diaphragm pumps, and its ability to operate even under intermittent conditions. The absence of mechanical seals is also an advantage in the transfer of process fluids, reducing the number of critical points prone to wear or leakage.
Why choose the FDA BOXER 100 as an industrial liquid pump
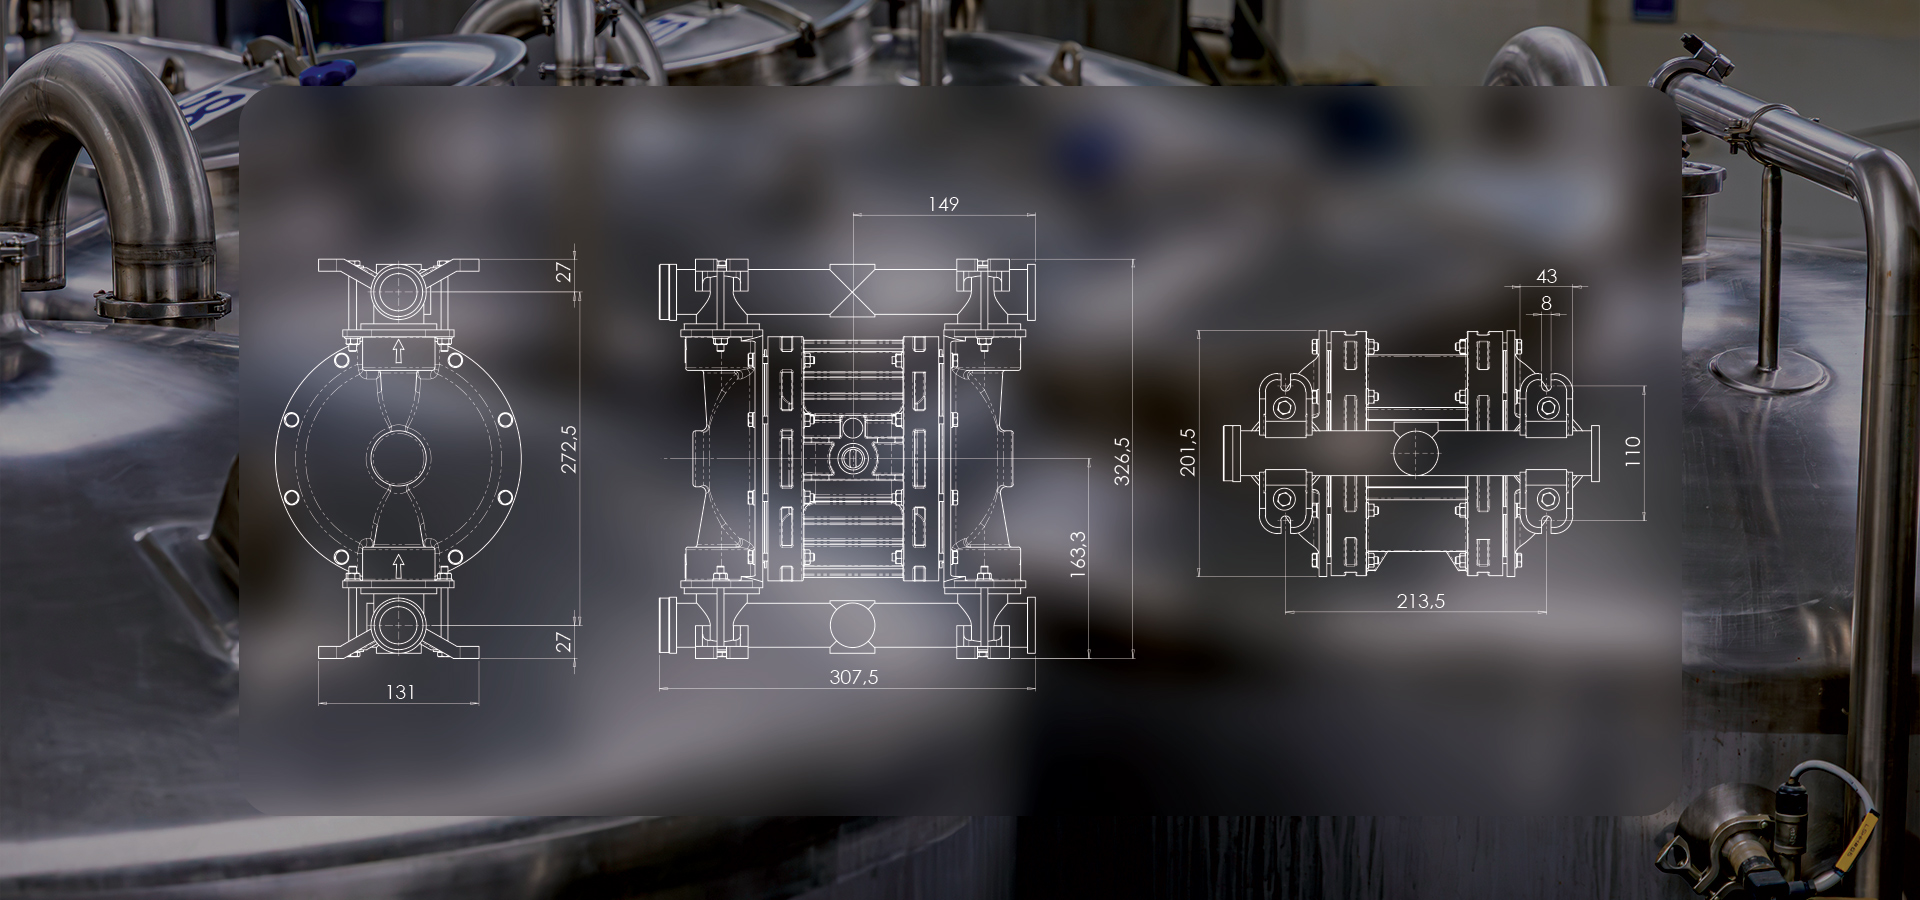
The company required a reliable and easily manoeuvrable stainless steel pump for industrial liquids, capable of handling n and discharge operations simply and safely. It was important to have a solution compatible with the flexible hoses, quick-connect fittings and process tanks already present in the plant, without requiring complex modifications to the existing installation. The choice of an FDA-compliant version stems from the need to use materials suitable for contact with fluids intended for sensitive applications, where the compatibility of components in contact with the product is a key requirement. The FDA BOXER 100 was therefore selected for its combination of reliability, versatility, ease of handling and the suitability of the materials in contact with the fluid.
Results achieved with the FDA BOXER 100 AODD pump for waste liquids
The installation of the FDA BOXER 100, successfully deployed as a double-diaphragm pump for waste liquids, has significantly improved the management of transfer operations within the plant. The mobile trolley configuration has made the pump easy to use at various points throughout the production area, increasing operational flexibility and simplifying operators’ tasks. The use of flexible hoses and quick-connect fittings has helped to make the connection and disconnection processes more practical, reducing system set-up times. Thanks to the pneumatic double-diaphragm technology and the FDA-compliant configuration, the solution has ensured reliable product transfer, contributing to operational continuity and the proper management of process fluids.
